
20+ years of professional and eco-friendly packaging manufacturing.
We follow strict glassware inspection precautions to ensure the highest quality. We must strictly reject glassware with breakage, cracks, chipping, or sharp edges that may cut hands. These precautions help us maintain safety and quality.
1. Glassware Inspection Precautions for Cracks and Deformation
Glassware must not deform. The rim and bottom must remain even, straight, and unwarped. We carefully check for any structural weaknesses.
2. Glassware Inspection Precautions for Material Purity and Thickness
Clear (flint) glass must not contain any recycled cullet. The product must appear transparent, pure white, and free of any off-color tints. For colored glass, the tone must be stable, pure, and uniformly consistent.
Whether produced by manual or machine blowing, the glass thickness must be uniform throughout. We do not accept uneven thickness (thick on one side and thin on the other). The glass batch must be well melted and homogeneous. We avoid defects such as stones (unmelted batch particles), cords (striae), and seeds (small bubbles) to the greatest extent possible.
3. Glassware Inspection Precautions for Bubbles and Annealing
We do not permit bubbles (seeds) larger than 1 cm above the rim (except for bubble-effect glass). Below the rim, there must be no more than two bubbles with a diameter greater than 2 mm. Also, there must be no more than three bubbles with a diameter greater than 1 mm. We also do not accept clusters of bubbles.
After de-molding, we must anneal the finished glass products for approximately 8 hours (minimum 6 hours) to ensure stable quality and prevent spontaneous breakage. Glass bottles and jars must possess adequate thermal shock resistance. When transferred from a hot water bath to a cold water bath, the temperature difference must generally be below 39°C. No breakage must occur during testing.
4. Glassware Inspection Precautions for Surface and Rim Quality
Both interior and exterior surfaces must not have prominent water marks (chilling marks). We do not permit surface defects that one can feel by hand, such as visible wrinkles, scratches, abrasions, shear marks, and mold seam lines. The surface must be free of cracks and incomplete filling defects.
The rim of the glassware must be smooth and even. It must be free of burrs, protrusions, and chipped edges.
5. Glassware Inspection Precautions for Cleanliness and Rust
Both the interior and exterior of the glassware must be clean. They must be free of foreign matter, dust, water stains, and glass debris. Rust stains must not appear on the glassware. The glass batch must not contain black specks, dust, or other impurities.
Note: Rust stains on glassware are typically caused by rust from tongs used during annealing or from rusty molds. This rust transfers onto the glass surface and cannot be removed afterward. Therefore, we must remove rust from tongs and molds before production commences. Additionally, we must take care during melting to prevent dust and impurities from falling into the batch. This would result in inclusions within the finished product.
6. Glassware Inspection Precautions for Decals and Etching
For acid-etched glass, we must strictly avoid contact with oil or grease prior to acid treatment. Otherwise, uneven etching may occur, resulting in localized glossy spots. After acid treatment, we must thoroughly clean residual white powder (acid residue) from both the interior and exterior surfaces.
For decal-applied products, the decals must be applied smoothly and evenly, without tilting or air bubbles. We generally require natural air-drying for 12 hours before firing. Residual water droplets may remain after soaking the decals. These droplets can vaporize during firing, rupture the decal film, and cause pinhole defects.
7. Glassware Inspection Precautions for Assembly and Packaging
Product dimensions must comply with specified requirements, and tolerances must not be excessive. If the product requires assembly with lids or other components, we must pay special attention to ensuring that the inner rim diameter meets assembly specifications.
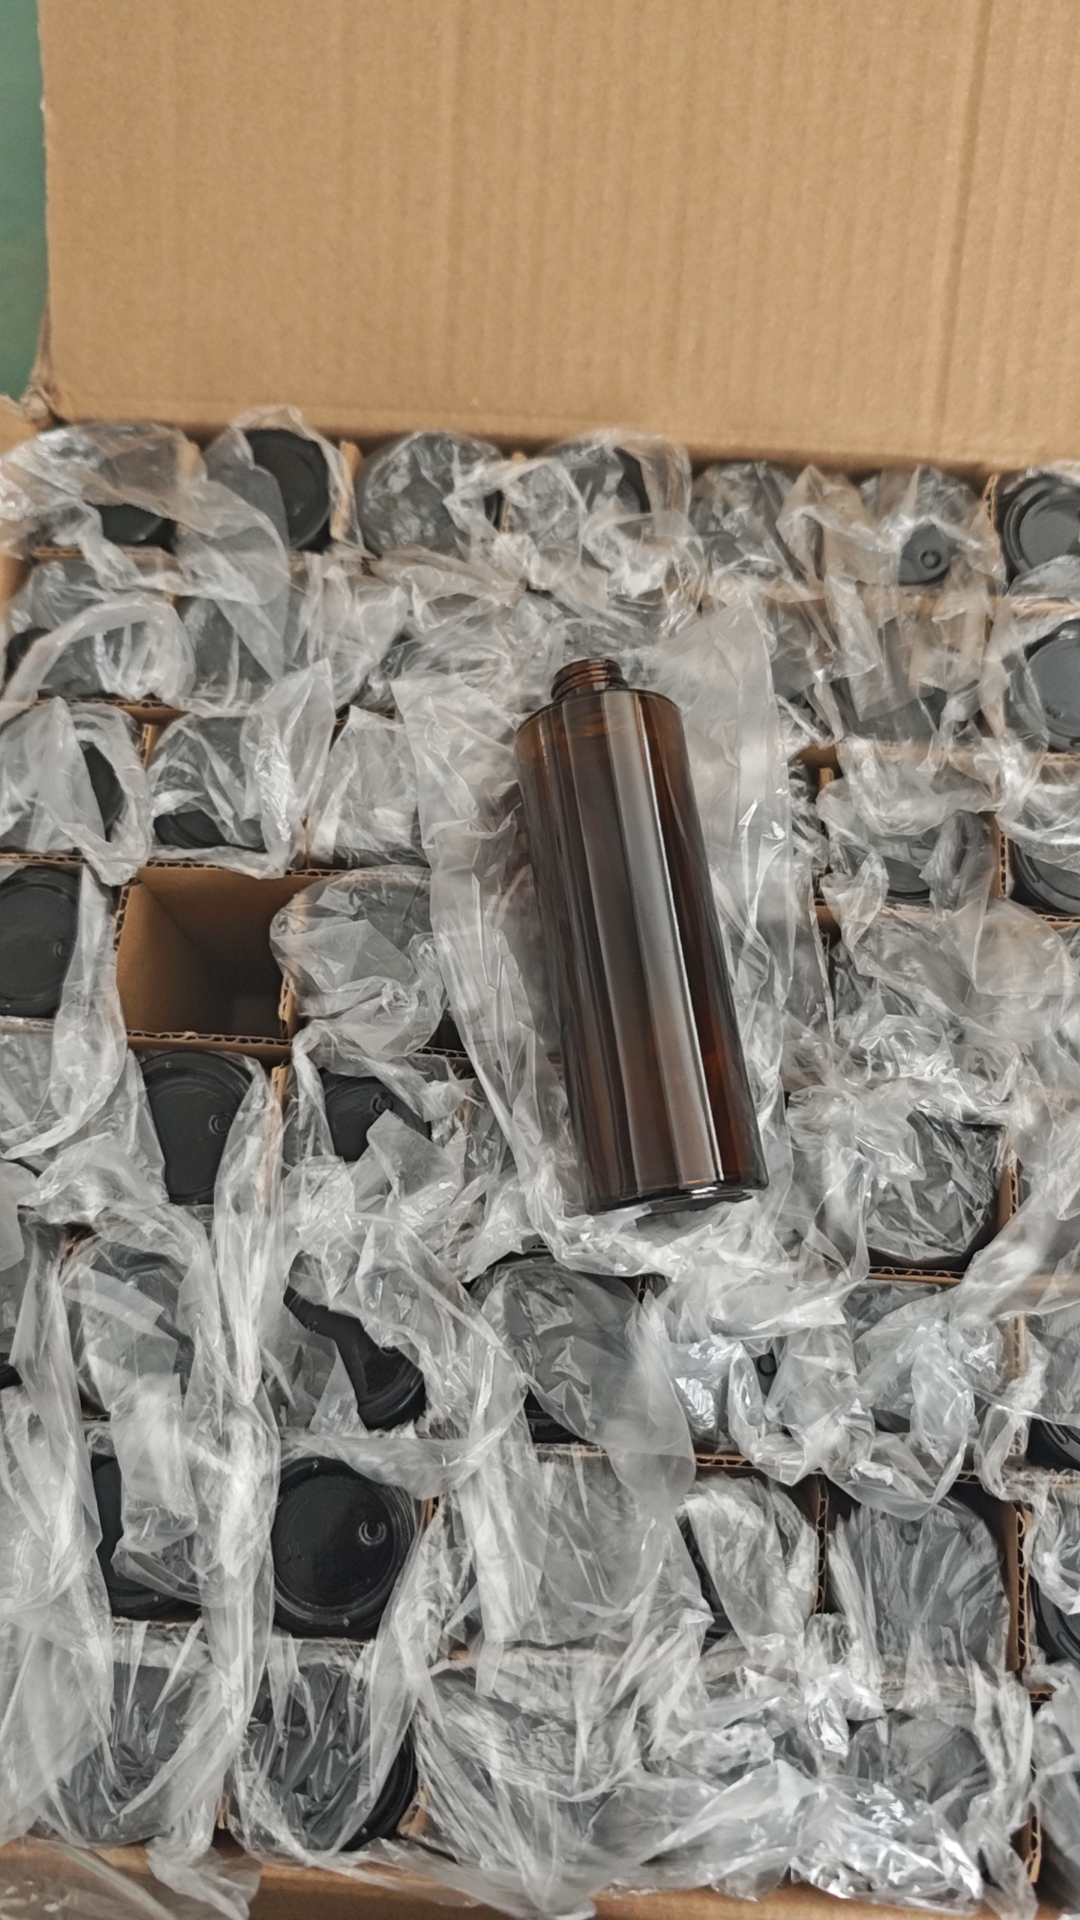
Glassware is fragile. During transportation, loading, and unloading, products must be stored and handled in an upright position. We must individually wrap each piece in paper and separate them with partition dividers (egg-crate inserts). This prevents impact and breakage from mutual collision. We will determine specific packaging methods according to the product type and order requirements. However, packaging safety is paramount. The packaging must be designed to prevent breakage during export shipment and ensure safe delivery to the destination.
During the inspection process, carefully verify the packaging method, labels and their content, accompanying instruction manuals, and inner/outer carton shipping marks for accuracy.
8. Final Glassware Inspection Precautions for Functionality
While appearance is important, the functionality of the product must be the foremost priority in inspection, regardless of the product type.
20+ years of professional and eco-friendly packaging manufacturing.
go back to news:https://www.diviniopackaging.com/index.php/category/news/
go back to homepage: https://www.diviniopackaging.com/
visit to our Instagram: https://www.instagram.com/divinio_packaging/
Facebook:https://www.facebook.com/profile.php?id=61550621670456
Linked:https://www.linkedin.com/in/guangzhou-divinio-packaging-products-co-ltd-45829a56/